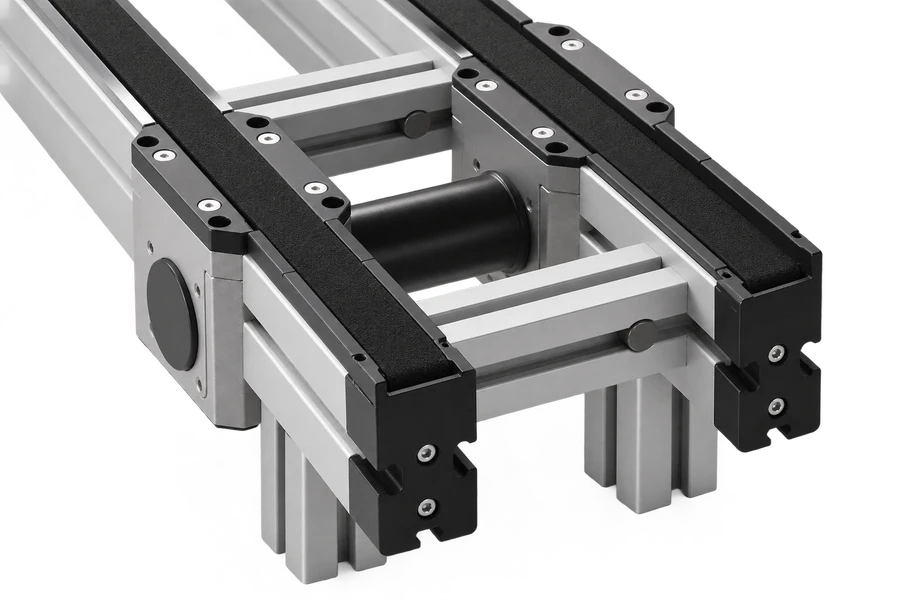
Timing Belt
Provides the conveying contact used to move the pallet through the conveyor section.
TOSH-1 PALLET CONVEYOR PLATFORM
TOSH-1 is a modular timing belt pallet conveyor, also referred to in the Toshine product catalog as a synchronous belt conveyor, designed for controlled workpiece-carrier transport between automated production and process stations.
Configured around the workpiece, pallet, process sequence and production-line layout.
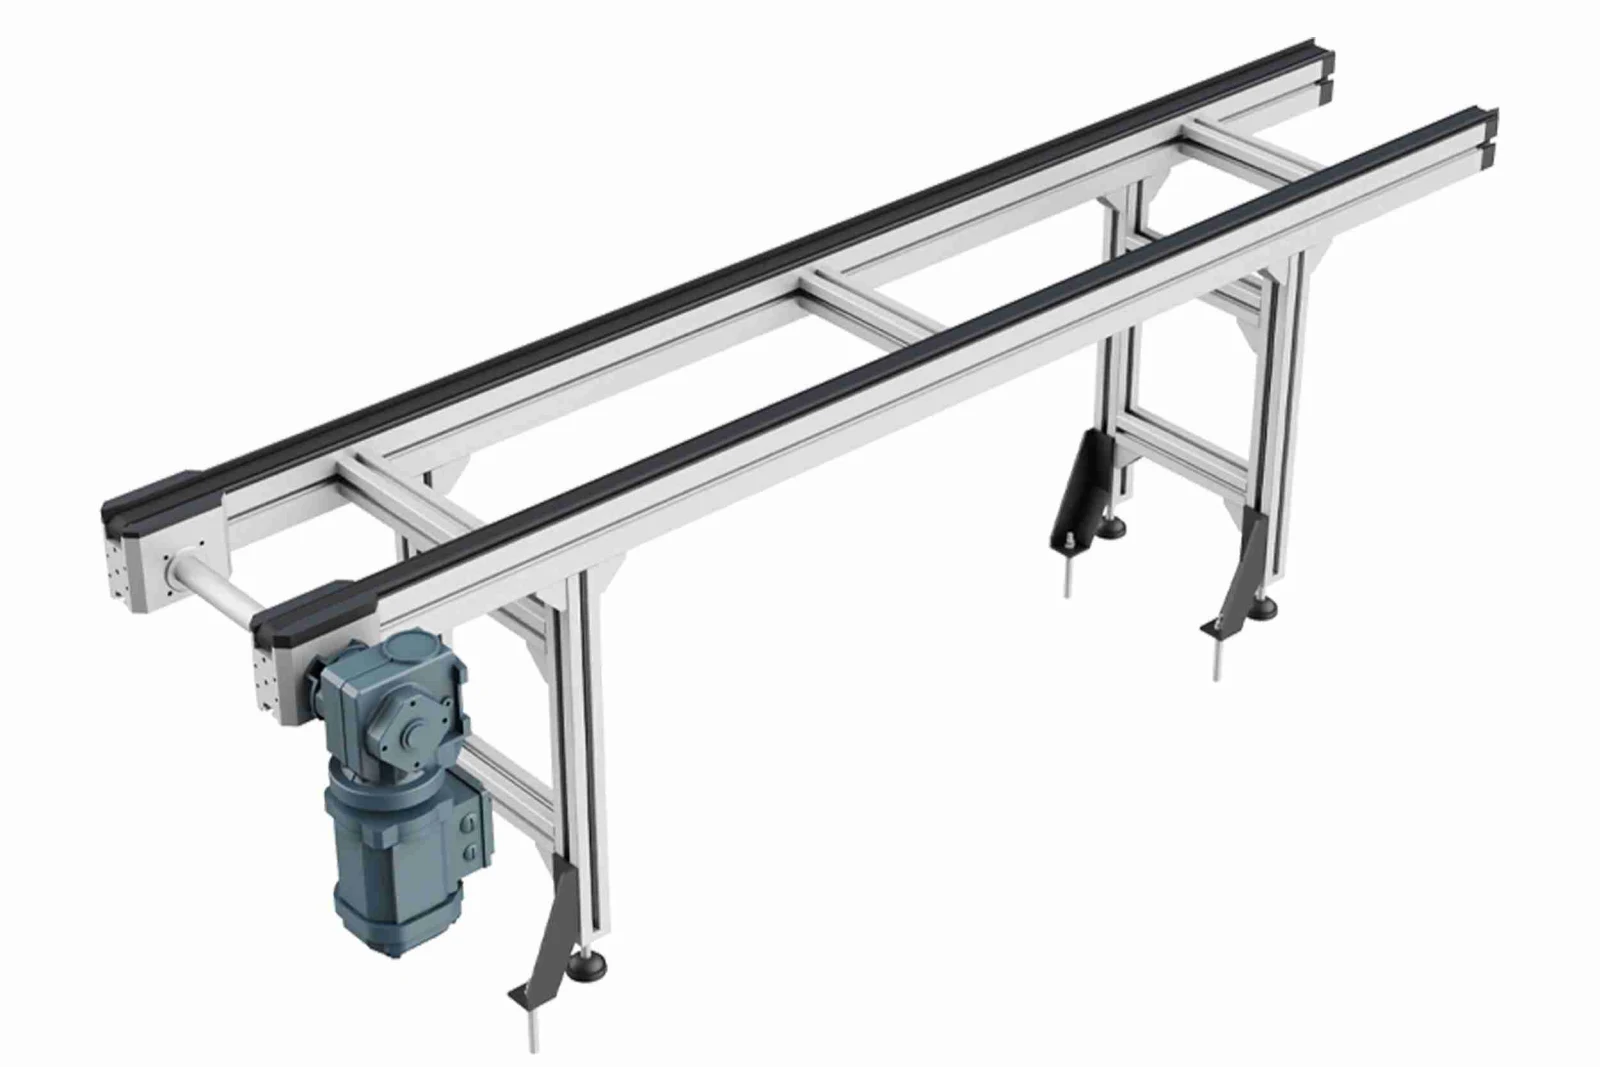
PRODUCT OVERVIEW
TOSH-1 transports pallets or workpiece carriers on a high-strength aluminum profile structure. It supports accumulation conveying and is available with end-drive or center-drive arrangements. Compatible curve, transfer, positioning, lifting and rotation modules can be evaluated around the production flow.
SYSTEM ANATOMY
The following elements provide pallet support, motion and structural integration.
Provides the conveying interface for stable pallet movement.
Carries the workpiece and can be configured around the fixture and process requirements.
Provides a modular structural platform for conveyor and automation integration.
End-drive or center-drive arrangement can be selected according to conveyor layout.
Moves the pallet between process stations as part of the production flow.
CONFIGURATION
Review these interfaces when configuring the conveyor section.
Provides the conveying contact used to move the pallet through the conveyor section.
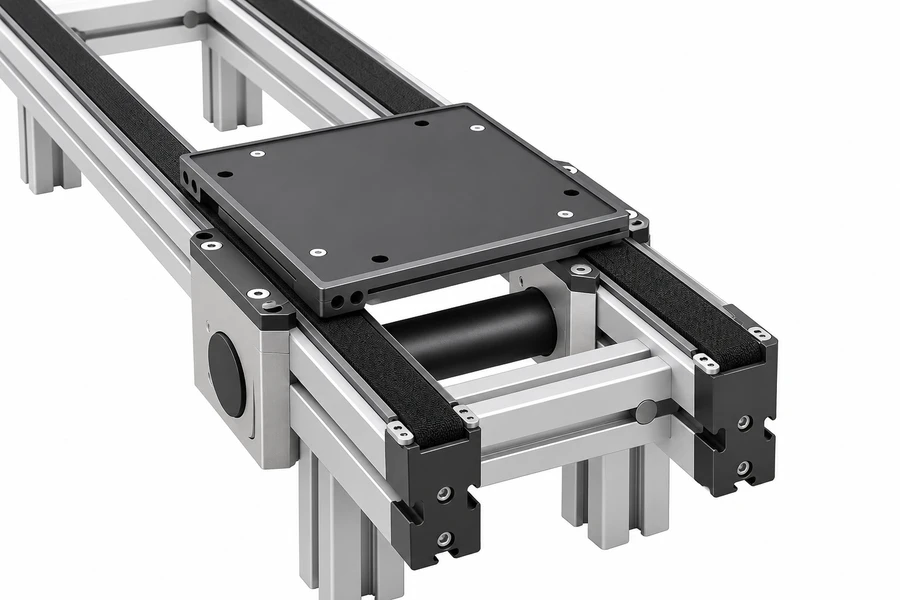
Supports the workpiece and its fixture while providing the carrier interface to the conveyor.
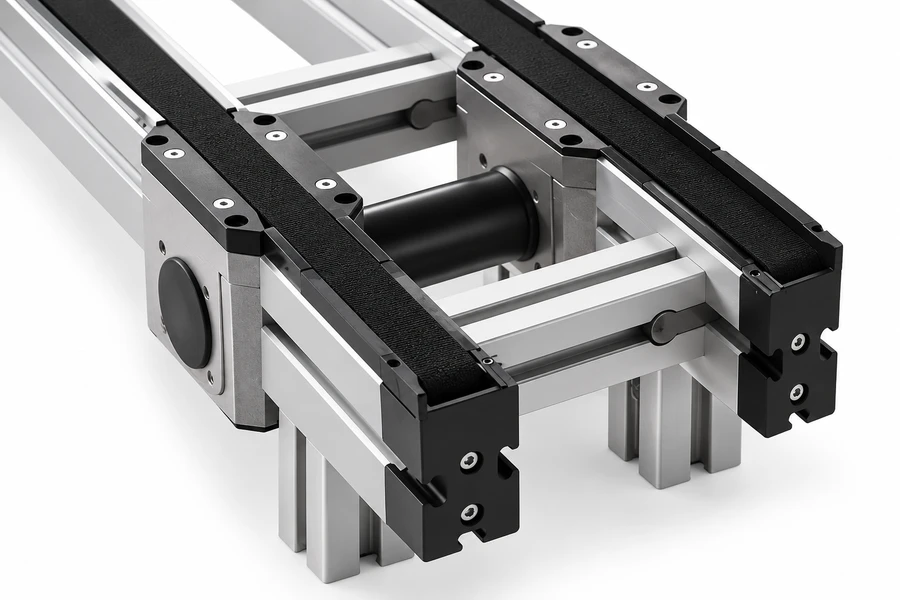
End Drive or Center Drive can be evaluated according to the conveyor layout and section arrangement.
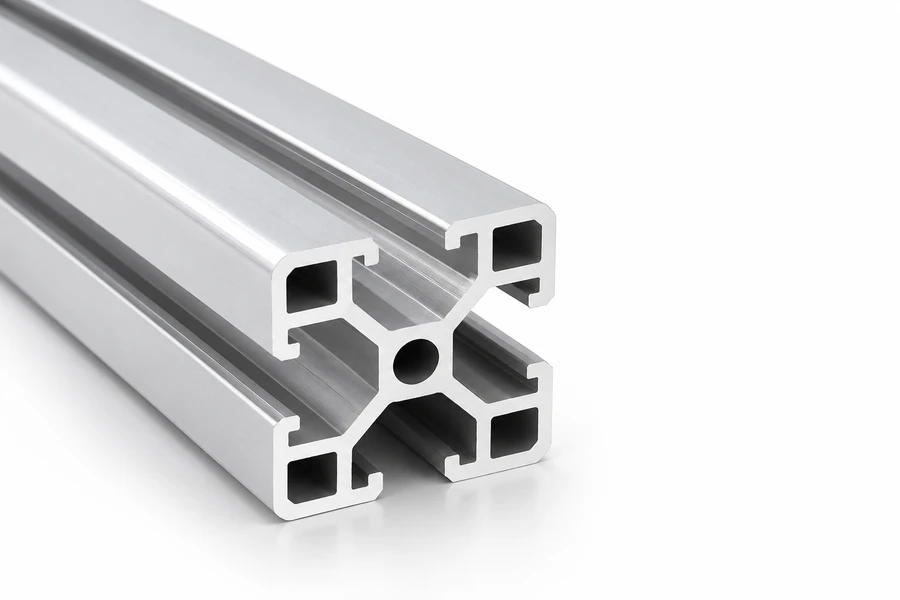
Forms the structural base for the conveyor section and surrounding automation interfaces.
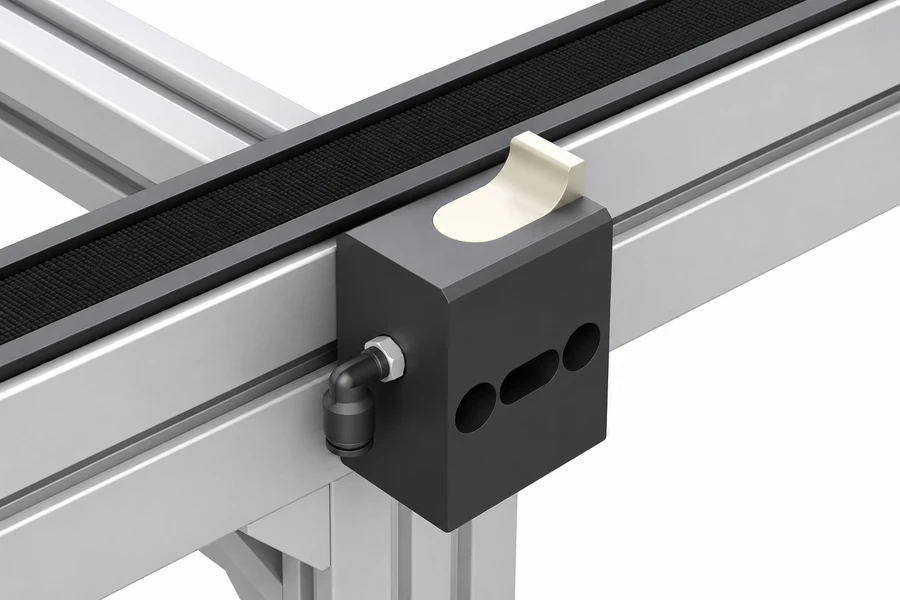
Supports controlled pallet release and location at a process station when the application requires it.
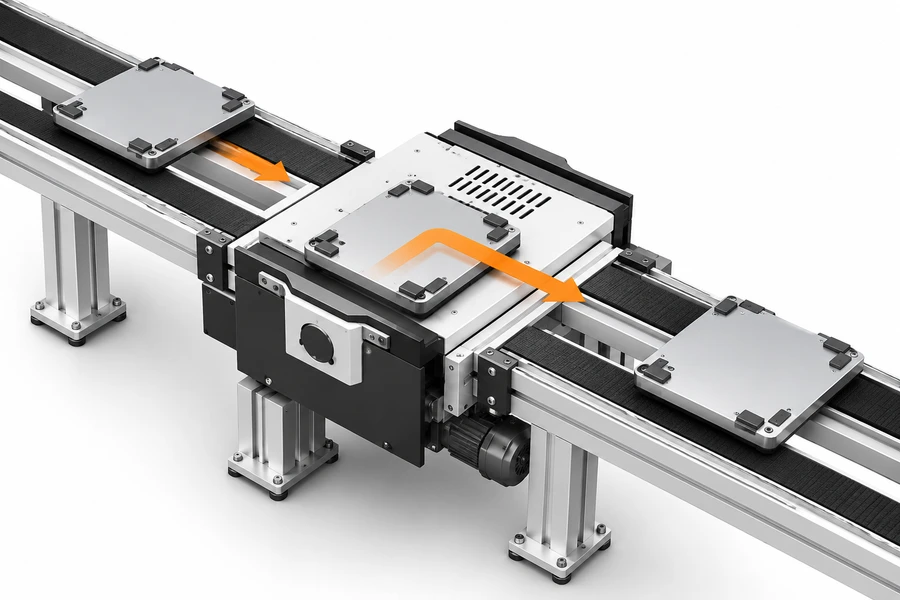
Connects conveyor sections, process directions or adjacent handling functions within the material flow.
DRIVE CONFIGURATION
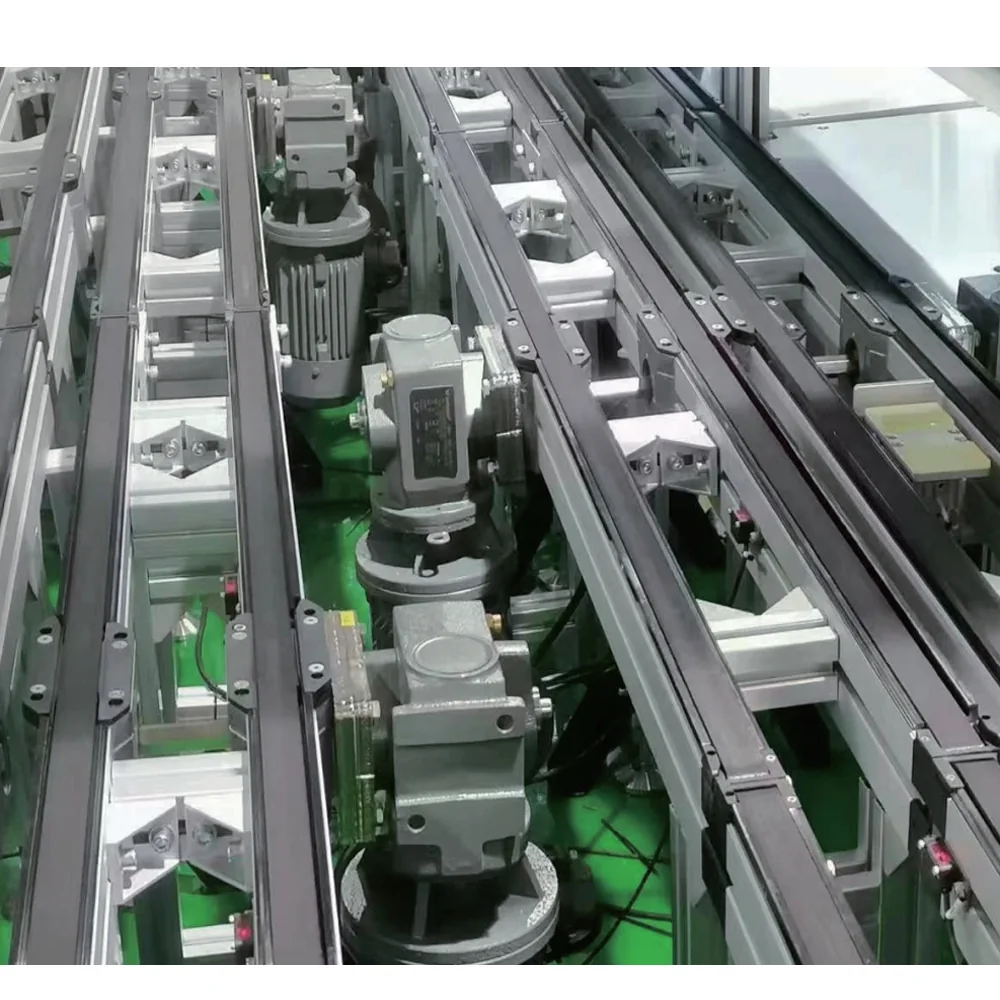
TOSH-1 can be configured with either end drive or center drive depending on conveyor length, layout and equipment arrangement.
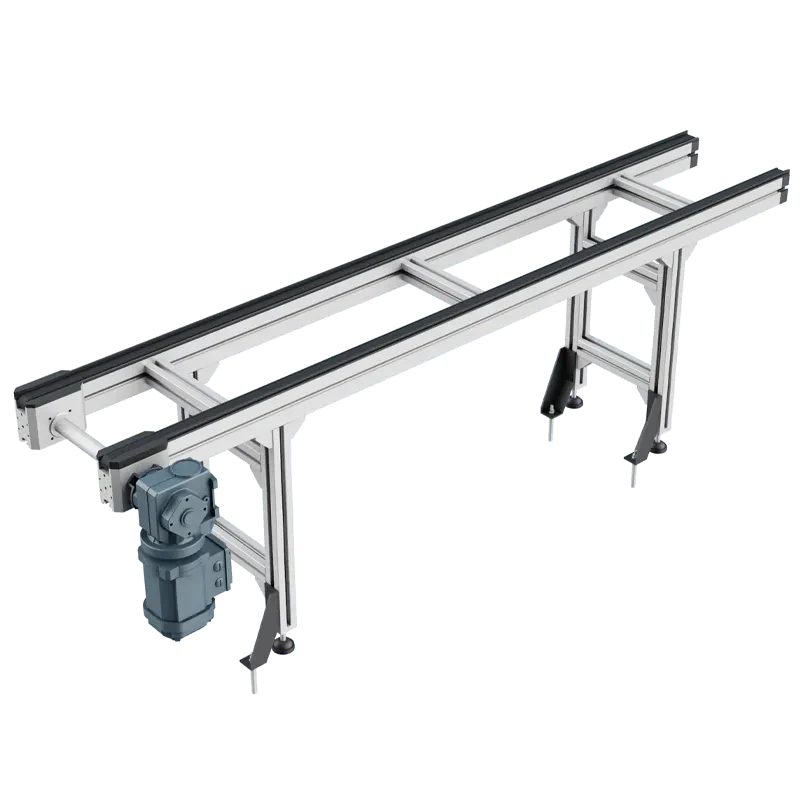
Motor and drive assembly positioned near the end of the conveyor section.
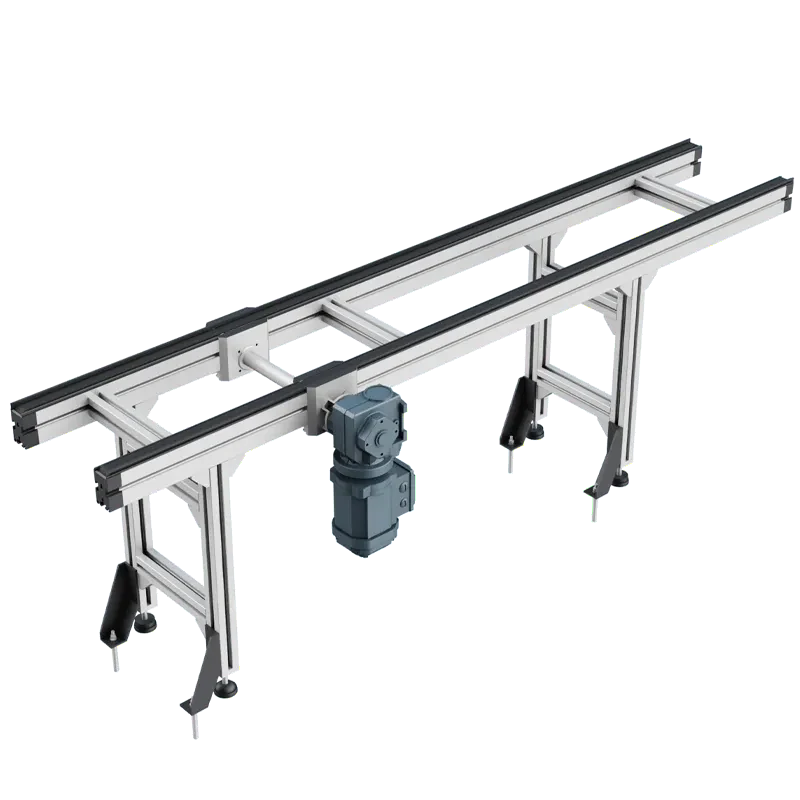
Drive assembly positioned within the conveyor section to support different layout and installation requirements.
TECHNICAL CONFIGURATION
Catalog values define the available product range. Final selection remains application-dependent.
| Model | TOSH-1 |
|---|---|
| Conveyor Type | Synchronous Belt Pallet Conveyor |
| Conveyor Length | 400–6000 mm |
| Pallet Width | 160–1200 mm |
| Conveying Height | As Needed |
| Conveyor Speed | Max. 20 m/min |
| Maximum Load Capacity | 60 kg |
| Drive Configuration | End Drive / Center Drive |
| Motor Position | Configured according to conveyor arrangement |
| Motor Direction | Configured according to conveyor arrangement |
| Noise | ≤60 dB at rated speed |
Reverse operation is possible, but conveying capacity is reduced compared with forward operation. Forward conveying is recommended for normal system design.
Final configuration is determined according to the workpiece, pallet, payload, process sequence, cycle requirements and production-line layout.
SELECTION FORMAT
TOSH-1 / L / W / H / V / Motor Position / Motor Direction
Catalog example:
TOSH-1 / L2340 / W320 / H900 / V12 / OP / F1Final configuration should be confirmed according to the pallet, workpiece, production process and line layout.
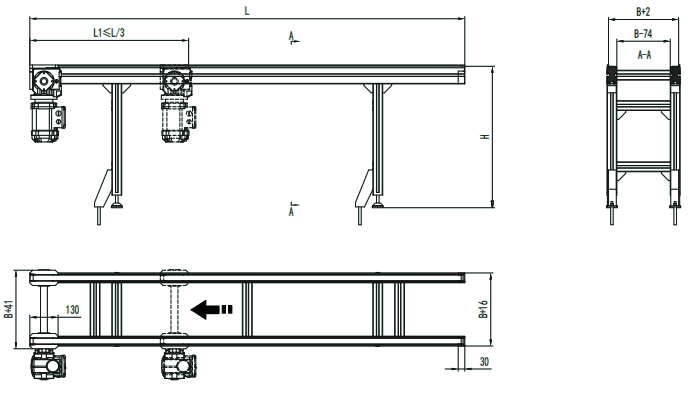
ENGINEERING DRAWING
Final dimensions depend on conveyor length, pallet width, conveying height and drive arrangement.
FUNCTIONAL MODULES
TOSH-1 conveyor sections can be combined with pallet handling modules to create application-specific material flow. Module selection is evaluated for each configuration.
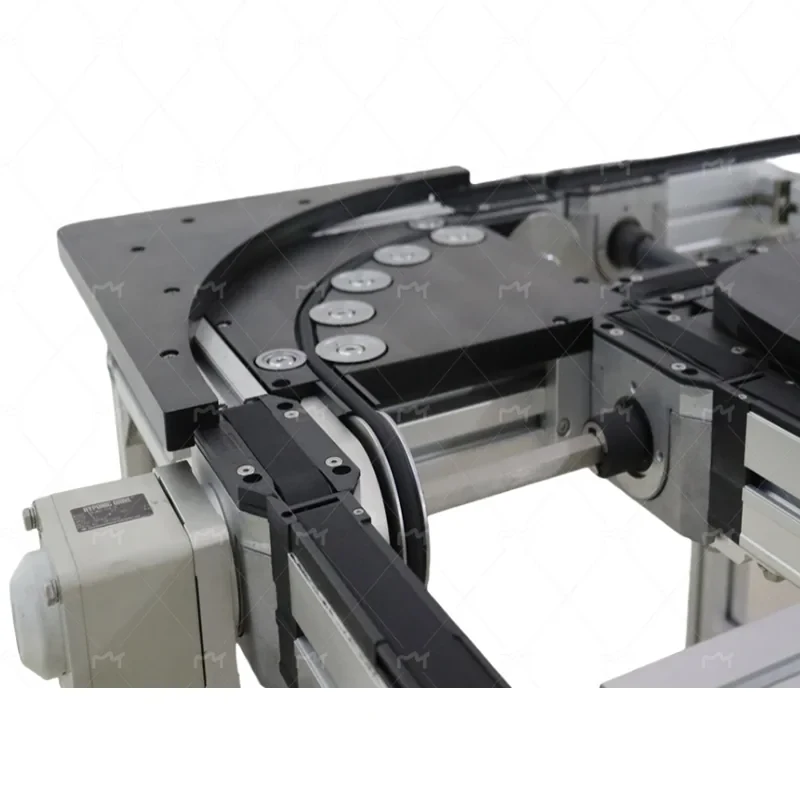
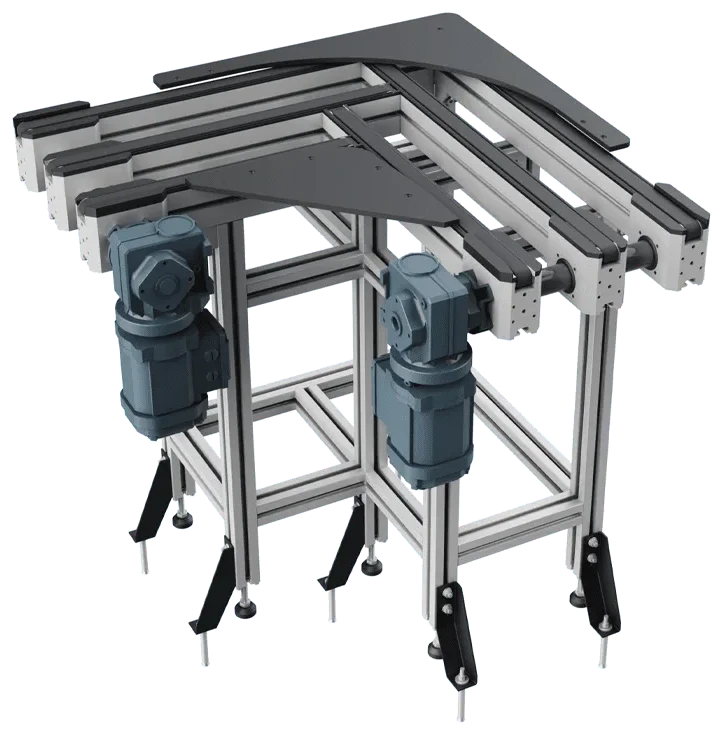
Changes pallet travel direction by 90°.
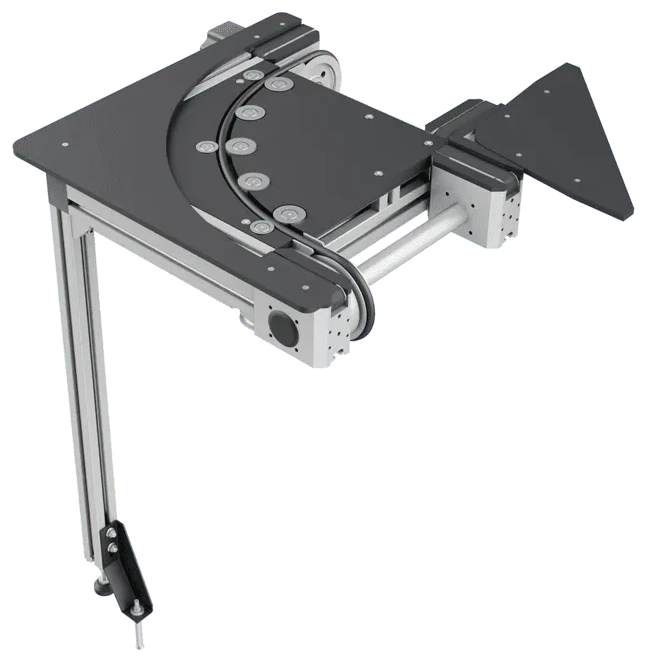
Provides a 90° pallet direction change using a round-belt curve mechanism.
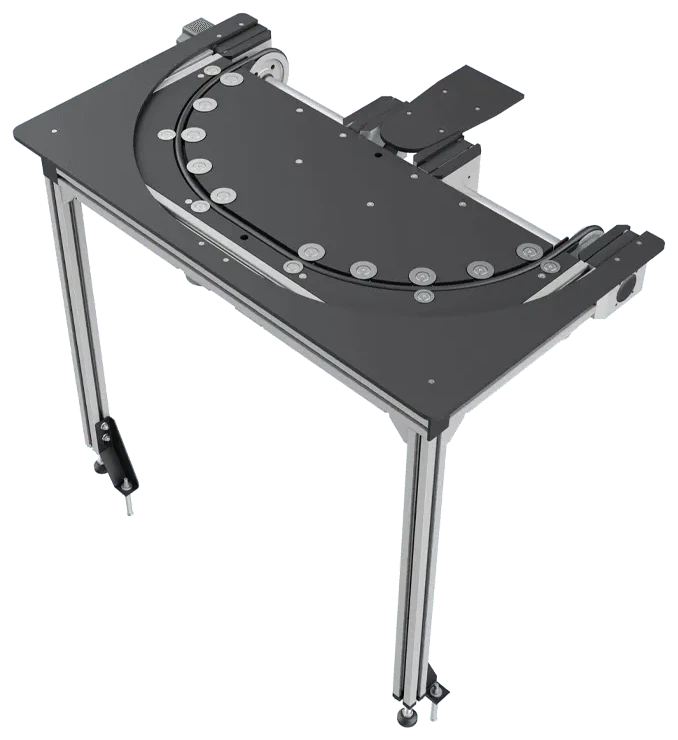
Provides a 180° pallet return / direction-change path.
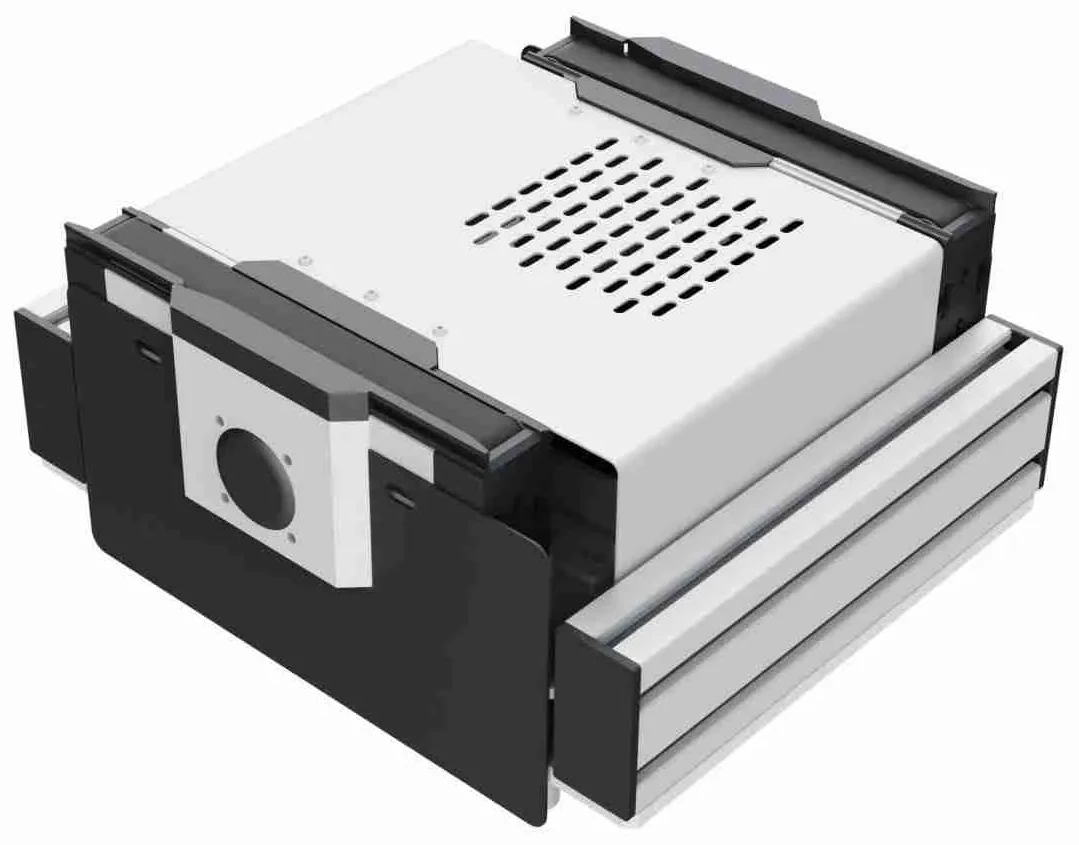
Transfers a pallet laterally by 90° between conveyor directions.
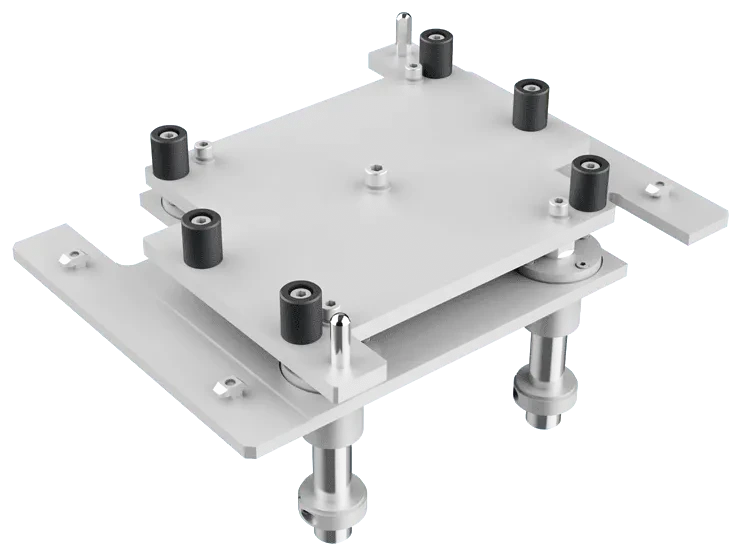
Raises and positions the pallet at a process station.
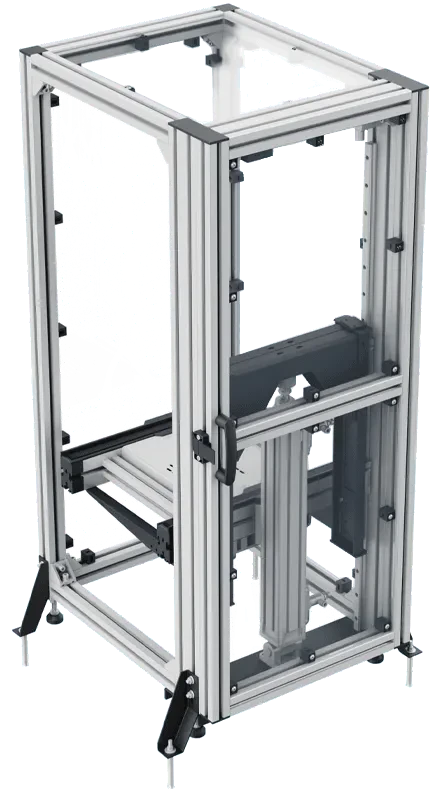
Moves pallets vertically between conveyor levels.
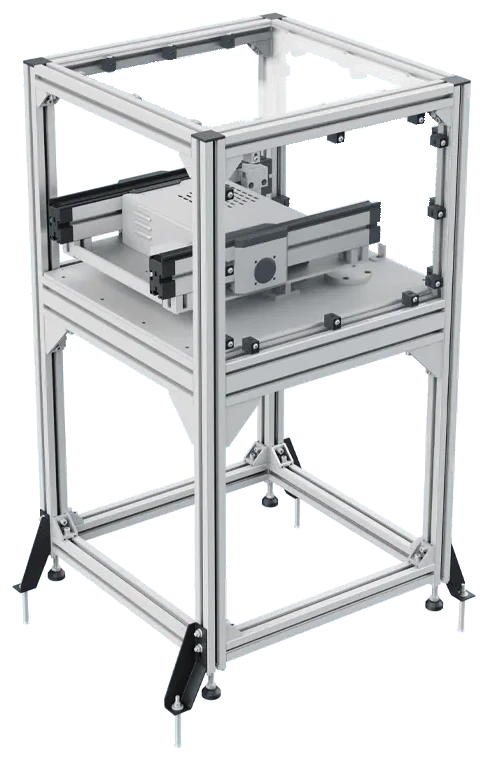
Rotates pallets for directional changes within the pallet handling system.
SYSTEM FLOW
Arrange compatible transport, transfer and positioning functions in the required process sequence.
APPLICATIONS
Application evaluation starts with the process operation and required workpiece movement.
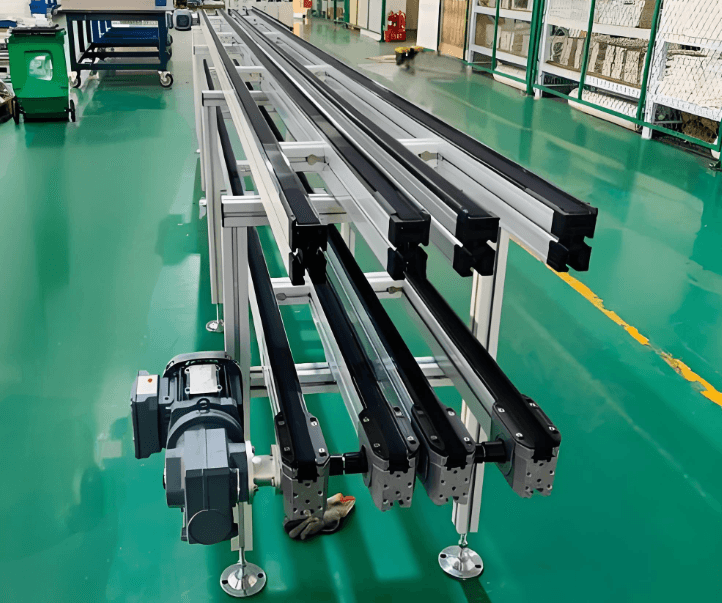
Pallet transport between assembly, inspection and testing processes.
Workpiece-carrier movement through multi-station assembly processes.
Controlled component transfer between automated production stations.
Pallet-based workpiece movement through sequential production processes.
PLATFORM SELECTION
Toshine has different pallet conveyor platforms for different workpiece, payload and process requirements.
Controlled transfer for compact workpiece carriers and multi-station automation.
CURRENT PRODUCTChain-based pallet transport for broader assembly-line applications.
For applications requiring a more robust chain conveyor platform.
Roller-based pallet transport for suitable pallet and workpiece configurations.
PROJECT INPUTS
Dimensions and characteristics
Existing pallet or required carrier concept
Workpiece + fixture + pallet
Assembly, testing, inspection or other operations
Straight, loop, transfer or multi-section arrangement
Required production flow / takt considerations
Required stopping and locating functions
Integration requirements with surrounding automation
ENGINEERING FAQ
Application-oriented answers without assumed performance values.
It is a conveyor platform that moves a pallet or workpiece carrier on timing belts between production stations. The carrier supports the workpiece while the conveyor provides the transport path.
TOSH-1 can be evaluated when controlled pallet transfer is required for compact workpiece carriers and multi-station automation. Final selection depends on the payload, carrier interface, process, layout and cycle requirements.
The pallet or carrier concept can be configured around the workpiece fixture and process requirements. Its final design requires review of the workpiece, support points, process access and conveyor interface.
Stop and positioning functions can be considered where a process station requires controlled pallet release or location. The required function and station interface must be evaluated for the application.
Transfer and direction-change functions can be considered as part of the material-flow layout. Compatibility and configuration depend on the pallet, route and required movement.
They describe the location of the drive arrangement within a conveyor section. Selection depends on the conveyor layout and section configuration; performance differences should be confirmed during project engineering.
Provide the workpiece, pallet or carrier, total payload, process sequence, layout, cycle requirement, positioning functions and automation interfaces where available.
PROJECT DISCUSSION
Share the available workpiece, carrier, conveyor and production-line information to start an engineering discussion. Not every item is required before inquiry.
Share the available information below. Items that are still open can be reviewed during the engineering discussion.
Send your requirements to info@sytoshine.com or visit our contact page. Online form submissions are not yet enabled.